· AtlasPCB Engineering · Engineering · 20 min read
PCB Assembly Process: A Manufacturer's Step-by-Step Guide to SMT, Through-Hole, and Mixed Technology
A complete walkthrough of the PCB assembly process from solder paste printing through final test — written from the production floor. Covers SMT reflow with real profile parameters, through-hole wave and selective soldering, DFA review, common defect root causes, and the cost drivers that engineers can control during design.
Quick Answer
The PCB assembly process transforms a bare fabricated board into a functional electronic circuit through a carefully sequenced series of manufacturing operations. For surface mount technology, the sequence is solder paste printing through a laser-cut stencil, automated pick-and-place component mounting, reflow soldering through a multi-zone oven with a controlled thermal profile, and automated optical inspection. Through-hole components follow with either manual or automated insertion, then wave soldering or selective soldering, depending on the board layout. Mixed-technology boards require careful process sequencing so that reflow operations do not disturb previously soldered through-hole components. The entire line is bracketed by inspection stages — solder paste inspection after printing, AOI after reflow, X-ray for hidden joints under BGA and QFN packages, and in-circuit or functional testing at the end. Assembly quality begins at the design stage: pad geometry, component spacing, fiducial placement, and panelization decisions made during layout directly determine yield on the production floor.
Reviewed by AtlasPCB Engineering Team
A bare circuit board is an impressive piece of manufacturing in its own right — precision-etched copper traces, carefully drilled vias, controlled impedance geometries, and a surface finish waiting to receive solder. But until components are mounted and soldered to that board, it has no function. It cannot amplify a signal, regulate a voltage, or process a single instruction. The PCB assembly process is where a fabricated board becomes an electronic system, and it is also where the majority of quality problems in electronics manufacturing originate.
At AtlasPCB, our assembly lines process boards ranging from simple single-sided prototypes with a dozen components to complex twelve-layer mixed-technology designs carrying over two thousand parts, including fine-pitch BGAs, 01005 passives, and through-hole power connectors. Every one of those boards passes through the same fundamental process sequence, adapted and optimized for its specific requirements. This article walks through that sequence from the manufacturer’s perspective, explaining not just what happens at each step, but why each step matters, what can go wrong, and what design decisions made weeks earlier on your workstation determine the outcome on our production floor.
How PCB Assembly Differs from PCB Fabrication
The distinction between fabrication and assembly is fundamental, yet it is frequently blurred in conversation. PCB fabrication creates the bare board substrate: etching copper traces, laminating multiple layers, drilling and plating holes, applying solder mask and silkscreen, and finishing exposed copper pads with ENIG, HASL, OSP, or another surface finish. The output of fabrication is a board that contains electrical pathways but no active or passive electronic components.
PCB assembly — commonly abbreviated as PCBA — is the subsequent process of populating that bare board with components and creating permanent electrical and mechanical connections through soldering. The two processes require fundamentally different equipment, materials, and expertise. A fabrication facility operates lamination presses, drilling machines, etching lines, and plating baths. An assembly facility operates solder paste printers, pick-and-place machines, reflow ovens, wave soldering systems, and inspection equipment. Many contract manufacturers offer both services under one roof, which simplifies logistics and reduces the risk of handling damage between stages, but the operations remain distinct.
Understanding this distinction matters because the design decisions that affect fabrication quality are different from those that affect assembly quality. Trace width, copper weight, and via aspect ratios are fabrication concerns. Pad geometry, component spacing, fiducial placement, and paste mask design are assembly concerns. A board can be perfectly fabricated and still fail assembly because of issues that were invisible during bare board inspection.
What Your Assembly Partner Needs Before Production Starts
The assembly process does not begin with solder paste on a stencil. It begins with a data review, and the quality of the data you provide determines how quickly your boards move from order entry to the production floor.
A complete assembly data package includes several files that work together. The Bill of Materials is the master document. It should list every component on the board with its reference designator, manufacturer part number, package type, value, and quantity. Positions marked Do Not Populate should be explicitly noted rather than simply omitted, because an omitted line is indistinguishable from a missing line. If you approve alternate parts, say so in the BOM. If you do not, say that too.
The pick-and-place file, also called a centroid file or XY data, provides the physical coordinates and rotation angle for every component. This file drives the placement machines directly. Errors in rotation, coordinate origin, or unit convention translate immediately into misplaced parts on the production floor. The most common centroid file error we encounter is a mismatch between the coordinate origin used in the design tool and the origin expected by our equipment. This is easily avoided by confirming that your centroid data references the same origin as your Gerber data and clearly stating the unit system.
Assembly drawings show component outlines on the board, polarity indicators for diodes and ICs, pin-one markings, and any special assembly notes. These drawings serve as a visual cross-reference for our technicians and are especially important for through-hole components that are inserted manually.
Finally, the Gerber files themselves are needed, particularly the paste mask layers. The paste mask defines the stencil apertures used for solder paste printing and must accurately reflect any aperture reductions you have specified for fine-pitch components.
TURNKEY PCB ASSEMBLY
Need a Reliable Assembly Partner?
AtlasPCB offers turnkey PCB assembly from prototype to production with DFA review, component sourcing, and full inspection.
Request Assembly Quote ›
Design for Assembly Review — The Step Most Engineers Skip
Most engineers are familiar with Design for Manufacturability review for the bare board, checking trace widths, annular rings, and drill-to-copper clearances. Fewer engineers apply the same rigor to Design for Assembly, and the consequences appear on the production floor as placement errors, solder defects, and yield losses that could have been prevented with a fifteen-minute design review.
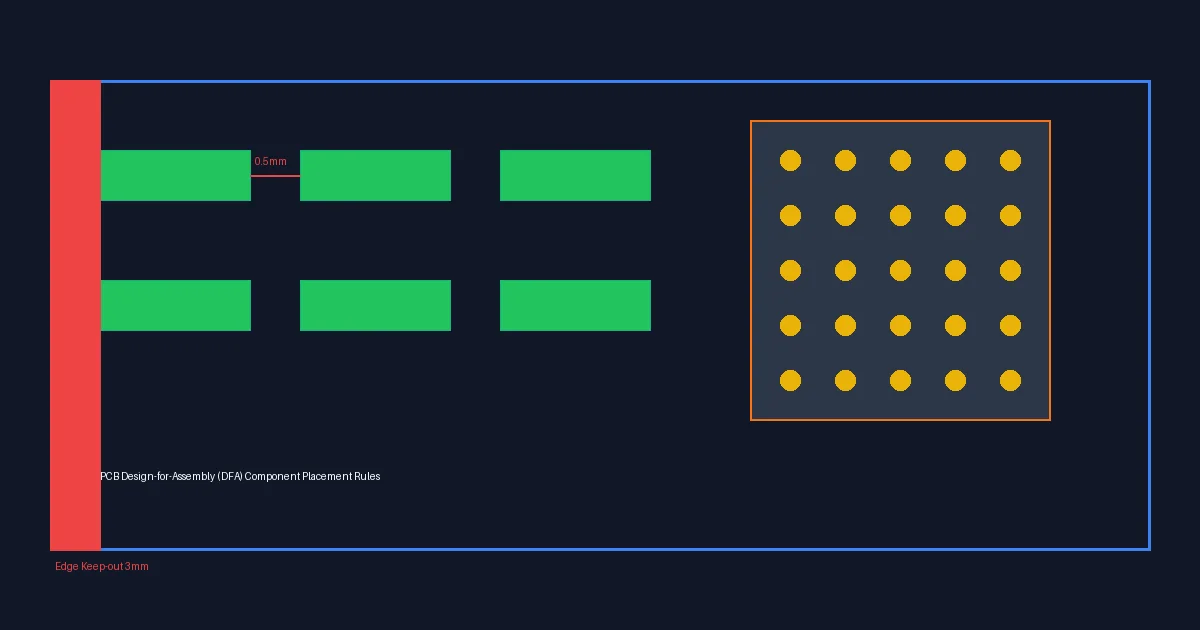
DFA review examines the assembled board from the assembly equipment’s perspective. Pick-and-place machines require a minimum clearance around each component to allow the vacuum nozzle to descend, place the part, and retract without disturbing adjacent components. When parts are spaced too closely, the nozzle may bump a neighboring component out of alignment during placement. The practical minimum component-to-component spacing for high-speed placement is 0.5 mm between body edges for standard packages, increasing to 1.0 mm when tall components are adjacent to short ones.
Fiducial marks are another DFA essential that designers sometimes omit. Global fiducials — typically three unmasked copper circles on the panel — provide the placement machine with optical registration references. Local fiducials placed near fine-pitch ICs and BGA packages give the machine additional position accuracy where it matters most. Without fiducials, the machine relies on board edge alignment, which introduces positioning errors that grow with board size. For boards carrying 0.4 mm pitch QFP packages or 0.5 mm pitch BGAs, local fiducials are not optional.
Panelization design also falls under DFA. Assembly lines handle panels, not individual boards, and the panel design determines how efficiently your boards can be processed. Rail width, breakout tab or V-score placement, panel fiducials, and tooling holes must all be considered during layout. A panel designed without consulting your assembler may require custom fixtures, reduce placement machine utilization, or create depaneling challenges that risk cracking solder joints near the board edge.
Solder Paste Printing and Stencil Design
The solder paste printing step deposits precise volumes of solder paste onto every SMT pad on the board. The process uses a laser-cut stainless steel stencil that is aligned to the panel and held in contact with the board surface while a squeegee blade forces paste through the stencil apertures. When the stencil separates from the board, each pad retains a controlled deposit of paste.
Stencil thickness is the primary variable controlling paste volume. A thicker stencil deposits more paste per aperture. For boards populated primarily with standard-pitch components — 0805, 0603, SOT-23, SOIC packages — a 5 mil (0.127 mm) stencil is the standard choice. When the board carries fine-pitch components with pad pitches below 0.5 mm, the stencil thickness must decrease to 4 mil or even 3 mil to prevent bridging between closely spaced pads. When the board also carries large connectors or power components that require substantial paste volumes, the stencil designer may need to use stepped stencils with different thicknesses in different regions, or apply aperture enlargement to the large pads on a thinner stencil.
After printing, modern assembly lines run every board through a solder paste inspection system. SPI uses 3D measurement to verify paste height, volume, area coverage, and position for every aperture on the board. This is arguably the most important inspection point in the entire assembly process, because paste printing defects — insufficient paste, excess paste, bridging, misalignment — are the root cause of the majority of solder joint defects downstream. Catching a printing defect before component placement means the board can be cleaned and reprinted at negligible cost. Missing that same defect after reflow means rework or scrap.
The paste volume window is tighter than most engineers realize. For a 0402 component, the acceptable paste volume per pad is approximately 0.02 to 0.04 cubic millimeters. Below that range, the joint lacks sufficient solder for reliable wetting. Above it, the excess solder increases the risk of bridging or tombstoning. For BGA pads at 0.5 mm pitch, the aperture is typically reduced to 80-90 percent of the pad diameter to control volume while maintaining consistent transfer efficiency.
Automated Component Placement
After paste printing and SPI verification, the panel moves to the pick-and-place machines. Modern high-speed placement equipment uses a rotating turret head or multi-spindle gantry to pick components from feeders, orient them using a vision system, and place them onto the paste-covered pads at speeds exceeding 40,000 components per hour for chip-scale parts.
Components arrive at the machine in different packaging formats. Passive components and small semiconductors come on tape-and-reel, which feeds through slots on the machine’s feeder bank. Larger ICs and connectors may arrive in JEDEC trays or tubes. The machine’s programming assigns each component to its feeder position and defines the nozzle type, placement force, and vision alignment method for each package.
Placement sequence matters. Most lines use a split approach: a high-speed chipshooter handles passive components and small semiconductors at maximum throughput, and a flexible placer handles large and odd-form components at lower speed but with greater versatility. The sequence is optimized to minimize head travel and feeder changes while ensuring that tall components are placed after short ones to avoid interference.
For fine-pitch and BGA packages, the placement machine uses its vision system to inspect each component before placement, verifying lead coplanarity, ball diameter consistency, and orientation. A BGA with one oxidized or missing ball is caught at this stage rather than discovered as a hidden defect after reflow. This pre-placement inspection is one of the capabilities that separates production-grade assembly from manual prototyping.
Reflow Soldering — Getting the Thermal Profile Right
Reflow soldering is the process that transforms paste deposits and placed components into permanent solder joints. The panel travels through a convection reflow oven with multiple independently controlled temperature zones, following a thermal profile that has been carefully developed and validated for the specific board and component combination.
A typical lead-free reflow profile for SAC305 solder alloy (the industry standard tin-silver-copper formulation) progresses through four distinct phases. The preheat ramp raises the board temperature from ambient to approximately 150 degrees Celsius at a rate of 1.0 to 2.0 degrees per second. Ramping too quickly risks thermal shock to sensitive components and uneven heating across boards with varying copper density. Ramping too slowly extends the total time in the oven and can degrade flux activity before reflow begins.
The thermal soak zone holds the board between 150 and 200 degrees Celsius for 60 to 120 seconds. This phase serves several purposes: it allows the entire board to reach thermal equilibrium, activates the flux to remove surface oxides from pads and component terminations, and drives off volatile solvents from the paste. Boards with large ground planes and heavy copper layers require longer soak times to equalize temperature between high-mass and low-mass regions.
The reflow zone pushes the temperature above the SAC305 liquidus point of 217 degrees Celsius, typically reaching a peak between 235 and 250 degrees Celsius. The time above liquidus should be controlled between 40 and 90 seconds. Too little time above liquidus produces cold or partially reflowed joints. Too much time promotes intermetallic growth, pad dissolution, and component damage. The peak temperature itself is constrained by the most temperature-sensitive component on the board — most ICs are rated to a maximum body temperature of 260 degrees Celsius for lead-free processing, leaving a relatively narrow process window.
The cooling phase brings the board back below solidification temperature at a controlled rate, typically 2 to 4 degrees per second. Faster cooling produces a finer grain structure in the solder joint, which generally improves fatigue resistance. However, cooling too rapidly can induce thermal stress in ceramic capacitors and BGA packages, potentially causing micro-cracks.
Developing and validating the reflow profile is one of the most technically demanding aspects of assembly engineering. Our process engineers use thermocouple-instrumented test boards that match the actual production board’s thermal mass and copper distribution to measure temperatures at multiple points simultaneously. The profile is adjusted until all measurement points fall within the target windows, and the validated profile is locked into the oven’s recipe system for the production run.
Through-Hole and Mixed-Technology Assembly
While surface mount technology dominates modern electronics assembly, through-hole components remain essential for many applications. Power connectors, certain transformers, high-current terminals, board-to-board connectors, and mechanical mounting hardware often require the superior mechanical strength of a through-hole solder joint. Many production boards use a mixed-technology approach, combining SMT components on one or both sides with through-hole components inserted from the top.
Through-hole components on a mixed-technology board are typically inserted after the SMT reflow cycle is complete. Manual insertion is common for prototype and low-volume production, while automated insertion equipment handles higher volumes. The inserted components are then soldered using either wave soldering or selective soldering.
Wave soldering passes the bottom of the board across a standing wave of molten solder. The wave contacts the component leads and barrel openings, filling the plated through-holes with solder and forming joints. Wave soldering is efficient for boards with many through-hole components concentrated in one area, but it requires masking or selective pallets to protect bottom-side SMT components from the solder wave. The wave soldering process also introduces additional thermal stress to the board and previously reflowed SMT joints.
Selective soldering addresses these limitations by applying solder only to specific through-hole locations using a programmable nozzle or miniature wave. This eliminates the need for pallets and masking, reduces thermal stress to the board, and works well for mixed-technology boards with scattered through-hole components. Selective soldering is slower than wave soldering on a per-board basis, but the elimination of pallet setup and the reduction in rework often make it more cost-effective for mixed-technology designs.
An emerging alternative is pin-in-paste, also called intrusive reflow, where solder paste is printed into the through-hole pads and components are inserted before the SMT reflow cycle. The reflow oven melts the paste and fills the barrel, forming through-hole joints simultaneously with the SMT joints. This technique eliminates the separate soldering step entirely but requires careful paste volume control and is limited to components that can tolerate the reflow thermal profile.
MIXED-TECHNOLOGY ASSEMBLY
Complex Mixed-Technology Board?
Our engineering team reviews your design and recommends the most cost-effective assembly process for your specific component mix.
Get a Free DFA Review ›Inspection and Quality Control at Every Stage
A reliable assembly line does not rely on a single end-of-line inspection to catch defects. Quality control is distributed across the entire process, with inspection gates positioned where they can catch specific defect types at the lowest cost of correction.
Solder paste inspection after printing is the first gate. As discussed above, SPI catches paste volume, height, and position deviations before any components are placed. Catching a paste defect at this stage costs nothing — the board is simply cleaned and reprinted.
After reflow, automated optical inspection examines every solder joint and component position on the board. AOI systems use multi-angle cameras and structured light to detect missing components, misaligned or rotated parts, polarity errors, solder bridges, insufficient solder, and tombstoned passives. Modern AOI systems achieve defect detection rates above 99 percent for visible joint types, but they have a fundamental limitation: they cannot see joints that are hidden beneath component bodies.
X-ray inspection fills that gap. BGA packages, QFN and DFN packages, and other bottom-terminated components form their solder joints beneath the component body, completely invisible to optical inspection. X-ray imaging reveals void percentages in BGA balls, bridging between adjacent balls, head-in-pillow defects where the ball did not fully merge with the paste deposit, and open joints. For boards carrying BGA packages, X-ray inspection is not optional — it is the only non-destructive method that can verify joint quality.
Electrical testing provides the final verification that the assembled board functions as designed. In-circuit testing uses a bed-of-nails fixture to contact test points on the board and verify component values, connection continuity, and isolation between nets. Flying probe testing uses movable probes to achieve similar coverage without a custom fixture, making it more practical for prototype and low-volume production. Functional testing powers the board and exercises its intended operation, verifying that the assembled product performs within specification under operating conditions.
Common PCBA Defects and Their Root Causes
Understanding the most common assembly defects and their causes helps engineers design boards that are inherently more manufacturable. Every defect has a traceable root cause, and most root causes connect back to decisions made during design or process setup.
Tombstoning, where a small passive component stands on end during reflow, is caused by an imbalance in the forces acting on the component as solder melts. When one pad wets before the other — due to unequal paste volume, asymmetric pad size, or uneven thermal exposure — the surface tension of the molten solder on the first pad pulls that end of the component upward before the second pad can anchor it. Prevention requires symmetrical pad design, equal copper connections to both pads (avoid routing a wide trace directly to one pad while the other connects through a thin thermal relief), and balanced paste deposition.
Solder bridging occurs when solder spans between adjacent pads, creating an unintended short circuit. It is most common on fine-pitch IC leads and closely spaced passive components. The root causes are excess paste volume, insufficient solder mask dam between pads, component misalignment during placement, and pad design that allows solder to flow between adjacent features. Stencil aperture reduction, proper SPI monitoring, and adequate solder mask dam width (minimum 0.1 mm for standard processes, 0.075 mm for advanced) are the primary controls.
Head-in-pillow is a BGA-specific defect where the solder ball on the component and the solder paste on the pad both melt during reflow but fail to merge, forming a visually normal but electrically unreliable joint. The typical causes are BGA package warpage during reflow, which lifts balls away from the paste at the critical moment, and surface oxidation on the balls that prevents wetting. This defect is particularly insidious because it is invisible to AOI and can only be detected by X-ray inspection or electrical testing.
Insufficient wetting, where solder fails to spread properly across the pad surface, is commonly traced to contaminated or oxidized pads, expired solder paste, inadequate flux activity, or a reflow profile with insufficient time above liquidus. The choice of surface finish directly affects solderability, with ENIG and immersion silver providing the best wetting performance for lead-free assembly.
What Drives PCB Assembly Cost
Assembly pricing is driven by a combination of factors that engineers can influence through design decisions. Understanding these cost drivers allows you to optimize your design for both performance and manufacturing economy.
Component count is the most direct cost driver. Every additional component adds placement time, increases the BOM cost, requires feeder positions on the machine, and creates another potential defect site. Reducing component count through careful design — eliminating unnecessary decoupling capacitors, consolidating resistor networks, using integrated ICs where discrete solutions are not necessary — directly reduces assembly cost.
The technology mix matters significantly. A board with only standard SMT components (0402 and larger passives, SOIC and QFP ICs) can be placed at maximum machine speed with standard nozzles and feeders. Adding fine-pitch BGAs requires X-ray inspection. Adding through-hole components requires a separate soldering step. Adding odd-form components like large connectors, heat sinks, or shielding cans may require manual placement. Each additional technology adds process steps and increases the per-board cost.
Double-sided assembly roughly doubles the processing time because the board must pass through the placement and reflow cycle twice, with the first side’s components secured by the surface tension of the solder joints during the second pass. Designing a single-sided board when possible is one of the most effective cost reduction strategies.
Volume drives unit cost through NRE amortization and setup efficiency. The stencil, machine programming, and process development are essentially fixed costs that are spread across the production run. A 100-piece prototype run carries these costs heavily, while a 10,000-piece production run amortizes them to near zero per board.
ATLASPCB
Ready to Get Your Boards Assembled?
Upload your BOM and Gerber files for an instant PCBA quote with DFA review, component sourcing, and full inspection included.
Get Your Assembly Quote ›
Moisture Sensitivity and Component Handling
One aspect of assembly quality that rarely appears in process overviews but causes real failures on the production floor is moisture sensitivity. Many IC packages — particularly BGAs, QFPs, and certain connectors with plastic bodies — absorb moisture from the ambient atmosphere over time. When these moisture-laden components enter the reflow oven, the rapid temperature rise vaporizes the trapped water, creating internal pressure that can crack the package, delaminate the die attach, or cause popcorning where the package visibly bulges.
The industry classifies components by Moisture Sensitivity Level from MSL 1 (unlimited floor life, no precautions needed) through MSL 6 (must be reflowed within the bake time, mandatory baking before use). Components at MSL 3 and above have limited floor life after their moisture barrier bags are opened — typically 168 hours for MSL 3, 72 hours for MSL 4, and progressively shorter for higher levels. If the floor life is exceeded, the components must be baked in a controlled oven at 125 degrees Celsius for a specified duration to drive out absorbed moisture before they can be safely reflowed.
Managing MSL compliance requires disciplined warehouse and floor-level processes: recording bag-open times, rotating stock, monitoring ambient humidity, and baking components when floor life has been exceeded. This is an invisible cost of assembly that designers should be aware of, particularly when specifying moisture-sensitive components on boards that will be assembled in small batches over extended periods.
From Design to Production Floor
The PCB assembly process is a chain of interdependent operations where the quality of each step depends on the quality of the step before it, and where many critical quality factors are determined not on the assembly line but on the engineer’s workstation during layout. Solder paste printing quality depends on stencil design, which depends on pad geometry, which was defined months earlier in your EDA tool. Placement accuracy depends on fiducial marks and component spacing decisions. Reflow quality depends on the thermal mass distribution across the board, which is a function of copper layer design and component placement density.
The most effective way to improve assembly yield is to engage your assembly partner early in the design cycle. A DFA review before your layout is finalized costs nothing and can prevent thousands of dollars in rework, yield loss, and schedule delays. At AtlasPCB, we offer complimentary DFA review on every assembly order, and we encourage customers to send us preliminary layouts for feedback before committing to fabrication. The fifteen minutes that review takes consistently saves days on the production schedule and produces boards that work correctly the first time they are powered on.
About AtlasPCB — We specialize in complex PCB manufacturing for HDI, RF, and high-reliability applications. Explore our PCB assembly services, or get an full PCB manufacturing capabilities . Every order includes free engineering review. Get your quote.
Reviewed by AtlasPCB Engineering Team — IPC-certified manufacturing specialists with 15+ years of production experience in HDI, RF, and high-reliability PCB fabrication. Content based on factory floor data and real customer design reviews.
Frequently Asked Questions
What is the difference between PCB fabrication and PCB assembly?
What files do I need to provide for PCB assembly?
What causes tombstoning during SMT assembly?
How much does PCB assembly cost?
- PCB assembly
- PCBA
- SMT
- through-hole
- reflow soldering
- wave soldering
- DFA
- pick and place
- PCB manufacturing